7 Critical Incoming Inspection Standards to Define Before Ordering
Many raw material quality disputes are created before the shipment ever leaves the supplier.
A batch arrives at your warehouse. Your quality team tests the material and finds that one parameter does not meet the expected requirement. You put the batch on hold or reject it. The supplier sends its Certificate of Analysis (CoA) and says the batch passed.
Then the discussion begins.
The supplier used one test method. Your laboratory used another. The supplier interpreted the specification differently. Your internal acceptance limit was never formally communicated. The batch may technically meet the supplier’s specification, while failing your internal requirement.
This is why incoming inspection standards should be defined before the purchase order is placed—not after the material arrives.
The objective is not to create unnecessary testing requirements. It is to make sure that both sides have the same definition of what constitutes an acceptable raw material.
Why Incoming Inspection Standards Should Be Defined Before Ordering
A raw material specification is more than a list of numbers.
For each critical parameter, there should be a clear understanding of what is being measured, how it is measured, and what result is acceptable.
Consider a simple example:
Assay: ≥95%
That looks straightforward, but several questions remain.
Which analytical method is used?
Is the result reported on an as-is basis or dry basis?
What reference standard is used?
What is the permitted analytical variation?
Is the supplier’s release method the same as the buyer’s incoming test method?
Without these details, two laboratories can produce different results from the same material.
For regulated industries, specifications and scientifically appropriate test procedures are an established part of quality systems. FDA guidance on specifications emphasizes that acceptance criteria should be supported by appropriate analytical procedures and justified quality requirements.
For ingredient procurement, the same practical principle applies: define the critical requirements before shipment rather than trying to resolve them after delivery.
1. Define the Critical Specification Parameters
The first step is identifying which parameters actually determine whether the material is acceptable.
Depending on the ingredient, these may include:
- Identity
- Assay or active content
- Marker compounds
- Moisture
- Water activity
- Microbiological limits
- Heavy metals
- Residual solvents
- Particle size
- Bulk density
- Appearance
- Solubility or dispersibility
- pH
- Carrier composition
- Foreign matter
Not every parameter needs the same level of control.
A procurement specification should distinguish between critical quality attributes and routine descriptive information.
For example, if an ingredient is being used in a moisture-sensitive probiotic formulation, water activity may be commercially important even if it is not the first parameter considered when purchasing the ingredient.
If the material is intended for a tablet formulation, particle size, bulk density, flowability, and compressibility may become more relevant.
The specification should therefore be connected to the actual application.
2. Agree on the Testing Method
One of the most common causes of incoming inspection disputes is not the result itself, but the test method.
Two laboratories can sometimes obtain different results because they use different analytical procedures, sample preparation methods, instruments, reference materials, or calculation approaches.
This becomes particularly important for botanical extracts and other complex materials.
For example, a buyer may specify a marker compound at a certain percentage but fail to define the analytical method. The supplier’s laboratory may use one validated method, while the buyer’s laboratory uses another.
When the results differ, each party may believe its result is correct.
The solution is to define the applicable test method in advance.
Depending on the material, the specification may reference:
- A recognized pharmacopoeial method
- An official standard
- A validated supplier method
- An agreed internal method
- A specific analytical technique
- A defined sample preparation procedure
The method does not necessarily have to be complicated. It simply needs to be clear enough that both sides understand how the result will be generated.
ICH Q6A also emphasizes the relationship between specifications, analytical procedures, and acceptance criteria when establishing quality requirements.
3. Define the Acceptance Criteria, Not Just the Target Value
A target value is not always an acceptance criterion.
Suppose the target moisture is 5%.
Does that mean the batch must be exactly 5%?
Probably not.
A practical specification might instead define a maximum, such as NMT 5.0%, or an acceptable range depending on the material and application.
The same principle applies to assay, particle size, water activity, bulk density, and other measurable properties.
Terms such as:
- Minimum
- Maximum
- Range
- NLT
- NMT
- Typical value
should not be used interchangeably.
“Typical” does not necessarily mean “guaranteed.”
A supplier may provide a typical value on a technical sheet, while the actual release specification uses a different acceptance range.
That distinction should be understood before purchasing.
4. Clarify Whether the CoA Is a Release Document or a Guarantee
A Certificate of Analysis is important, but a CoA should not automatically be treated as the entire quality agreement.
A CoA normally reports test results for a particular batch against defined specifications. It provides useful batch-level information, but its meaning depends on the underlying specification and testing system.
This is why buyers should review what the CoA actually contains.
At minimum, consider whether it identifies:
Product name
Batch or lot number
Manufacturing or testing date
Specification limits
Actual test results
Testing methods where relevant
Release status
Supplier or manufacturer information
The batch number is particularly important because it connects the document to the physical material.
A CoA without clear batch identification is much less useful for traceability.
FDA’s dietary supplement CGMP framework requires specifications for components, in-process materials, packaging, and finished products, along with appropriate testing or examination procedures.
The practical procurement lesson is simple: do not ask only, “Can you provide a CoA?”
Ask, “What specification does this CoA demonstrate compliance with?”
5. Decide What Happens If Your Incoming Test Differs From the Supplier’s CoA
This point is often ignored until there is already a problem.
Imagine that the supplier’s CoA reports an assay of 98.2%, but your laboratory reports 94.8%, while your specification requires ≥95%.
What happens next?
If the purchase agreement never addressed this situation, both sides may start arguing from their own testing systems.
A more robust quality process defines the dispute procedure in advance.
For example, the agreement may specify:
Review the original supplier test result.
Confirm the batch and sample identity.
Review the analytical methods used by both laboratories.
Check sample handling and storage conditions.
Retest according to the agreed method.
If necessary, send a retained or mutually agreed sample to an independent laboratory.
The exact procedure will depend on the ingredient, risk level, contract, and quality system.
The important point is that disagreement should trigger a predefined process—not an improvised argument.
6. Make Batch Traceability Part of Incoming Inspection
Incoming inspection is not only about whether a test result passes.
It is also about knowing exactly which material was tested.
A proper receiving process should connect:
Purchase order → supplier → product → batch/lot number → CoA → physical shipment → test result → receiving decision.
This chain becomes particularly important when a supplier ships multiple batches of the same ingredient.
If a problem appears later, the buyer needs to know which batch was affected and what documentation supported its release.
For regulated food and supplement operations, traceability and recordkeeping are important elements of the broader quality system. FDA’s dietary supplement CGMP requirements include requirements around specifications, records, and documentation of component controls.
For procurement teams, the operational benefit is equally practical: good batch traceability makes investigations faster and reduces uncertainty when a quality issue occurs.
7. Define Which Requirements Are Mandatory Before You Request a Quote
Another common mistake is asking for a quotation first and discussing quality requirements later.
Price is only meaningful when the quoted material meets the technical requirement.
For example, two suppliers may both quote “Xylitol Powder,” but one may offer a standard particle size, while the other can supply a narrower particle-size range and lower water activity.
The prices cannot be compared fairly without first understanding the specification.
A better sourcing request separates requirements into three categories.
Mandatory:
Requirements that must be met, such as assay, identity, regulatory status, prohibited ingredients, or a specific water-activity limit.
Preferred:
Characteristics that would improve formulation or processing but may have acceptable alternatives.
Flexible:
Parameters where the buyer is willing to consider supplier recommendations.
This gives suppliers room to propose technically suitable alternatives without weakening the core quality requirements.
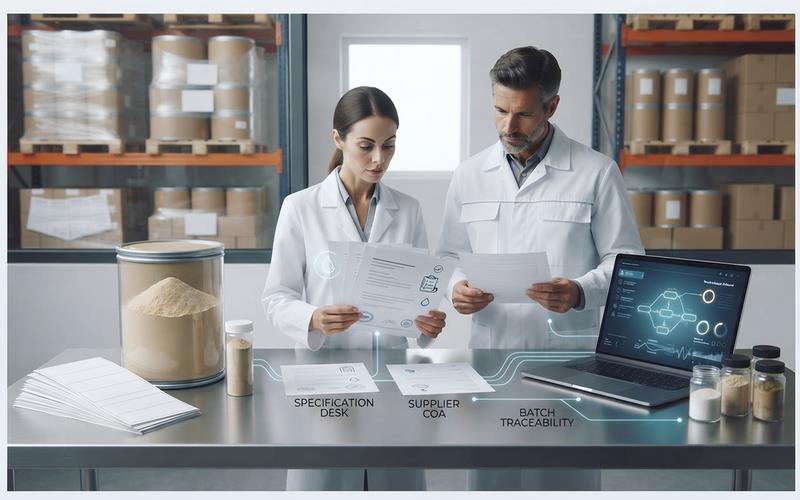
Incoming Inspection Should Start With the Purchase Specification
The best incoming inspection process does not begin when the truck arrives.
It begins when the purchase specification is created.
Before placing an order, procurement, R&D, quality, and the supplier should ideally have a common understanding of:
- What material is being purchased
- Which parameters are critical
- Which test methods apply
- What acceptance limits will be used
- What documentation must accompany the shipment
- How batch identification will be handled
- What happens if results disagree
This does not require every buyer to create a complicated quality agreement for every kilogram of raw material.
The level of detail should reflect the material’s risk, application, volume, regulatory requirements, and relationship with the supplier.
For a routine standard ingredient, a clear specification and batch CoA may be sufficient.
For a critical active ingredient, a moisture-sensitive raw material, a customized specification, or a high-value commercial batch, more detailed requirements may be appropriate.
Do Not Confuse Supplier Specifications With Your Own Requirements
A supplier’s standard specification is a useful starting point, but it does not automatically become the buyer’s specification.
This distinction is especially important when purchasing ingredients from multiple suppliers.
Supplier A may define moisture as NMT 5%.
Supplier B may define moisture as NMT 7%.
Both suppliers may consider their products compliant with their own specifications.
But if your formulation requires NMT 5%, only one of those specifications matches your requirement.
The same issue can occur with particle size, assay, microbiological limits, heavy metals, carrier composition, or water activity.
This is why supplier qualification and raw material qualification should include a review of the actual requirements of the buyer—not simply whether the supplier has a specification document.
A Practical Pre-Order Checklist
Before approving a raw material purchase, ask five simple questions:
1. What exactly are we buying?
Confirm identity, source, grade, form, and application.
2. What makes this batch acceptable?
Define critical parameters and acceptance criteria.
3. How will those parameters be tested?
Agree on analytical methods where differences could affect the result.
4. What documentation will arrive with the batch?
Confirm CoA, MSDS/SDS, specification, and other required documents.
5. What happens if our result disagrees with the supplier’s result?
Define the review, retesting, and resolution process before the shipment arrives.
These five questions can prevent a surprising amount of procurement friction.
Define “Acceptable” Before the Material Arrives
Most incoming inspection disputes are much harder to solve after the material is already sitting in a warehouse.
By that point, freight has been paid, production may be waiting, samples may already have been distributed, and both parties may be interpreting the documentation differently.
The better approach is to move the definition of “acceptable” upstream.
At Esubio, we support ingredient sourcing projects where specification alignment is important, including projects involving specific quality parameters, special specifications, low water activity, particle size, documentation requirements, and other application-related needs.
Depending on the ingredient and supplier, each shipment can be supported with batch-level documentation such as CoA, MSDS/SDS, and product specifications. Before ordering, we can also communicate with suppliers about key parameters and acceptance requirements so that the sourcing target is clearer from the beginning.
A supplier’s CoA should not be the first time a buyer sees the quality requirements.
The more important document is the specification agreed before the order.
When both sides define the same meaning of “acceptable” before shipment, incoming inspection becomes what it should be: a verification process—not a negotiation after the fact.
References
- FDA — Q6A Specifications: Test Procedures and Acceptance Criteria for New Drug Substances and New Drug Products
FDA Q6A — Specifications, Test Procedures and Acceptance Criteria - FDA — Current Good Manufacturing Practice, Hazard Analysis, and Risk-Based Preventive Controls for Human Food
FDA — Current Good Manufacturing Practice for Human Food - FDA — Dietary Supplement CGMP Compliance Program
FDA — Dietary Supplement Compliance Program - FDA — 21 CFR Part 111: Current Good Manufacturing Practice in Manufacturing, Packaging, Labeling, or Holding Operations for Dietary Supplements
FDA — 21 CFR Part 111